Wrench Time Analysis: How We Reduce Stamping Hammer Lifting Time from 45 to 21 Minutes
Since 1910 when a concept called time and motion study was designed for production assembly workers. A wrench time analysis provided valuable insight into where the main hours are being spent and how it can be improved. The concept if Wrench time is the actual time taken for the job as against the total time spent. It is the time spent by the maintenance staff on actually repairing the machine.
Wrench Time refers to the time maintenance technicians spend directly working on equipment, including repairs, replacing parts, and carrying out maintenance activities. It excludes the time spent collecting tools and spare parts, getting instructions, waiting for materials, and travelling to the job location.
To tell you the example: If a technician works an 8-hour shift and spends 3 hours arranging tools and spare parts, and travelling to the job location, the remaining 5 hours spent directly on equipment maintenance is considered Wrench Time. The thing is, wrench Time does not include break time. Other activities, such as collecting tools, arranging spare parts, and travelling to the job location, are necessary to complete the work, but they are not included in Wrench Time. Proper planning helps maintenance technicians work more efficiently during repairs.
Elements:
- Wasteful Activity
- Incidental Activity
- Wrench Time
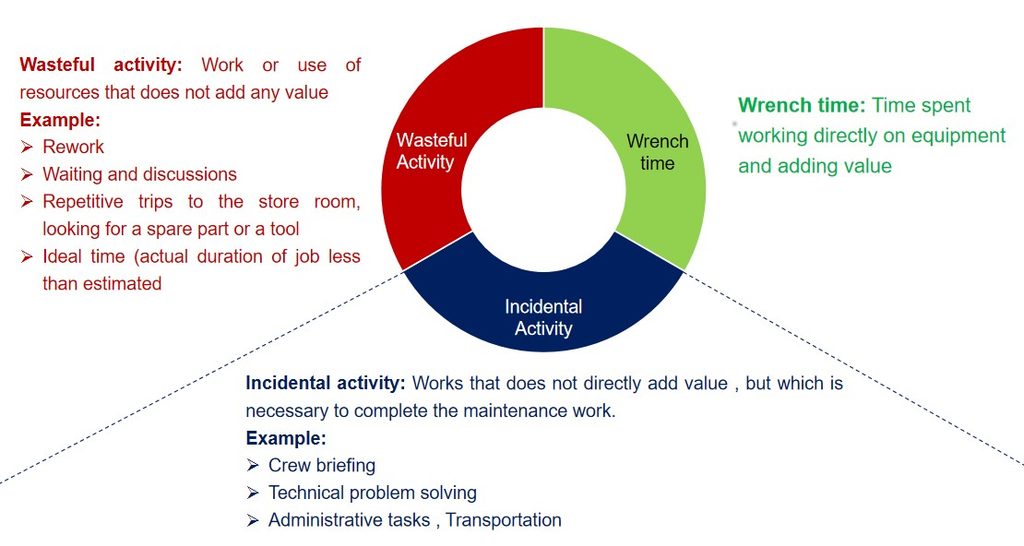
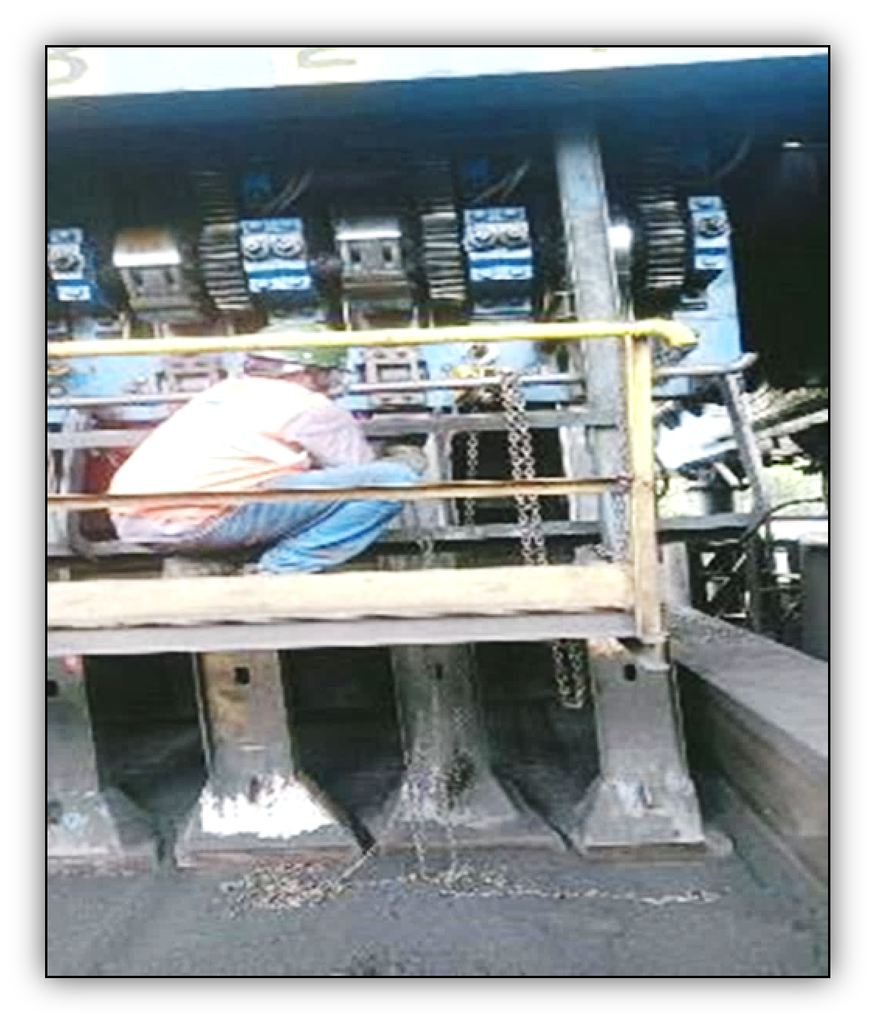
U can clearly Understood by this example
In our plant, two stamping stations are available. The stamping station is a critical area where a 55 MT coal cake with a bulk density of 1.17 kg/m³ is prepared using a hammering mechanism. The coal is compacted by dropping hammers up and down inside a closed box.
Each stamping station consists of two sets of hammers, with six hammers in each set. These hammers are used to prepare the coal cake. The hammers are made of I-beams lined with friction plates. The hammers may need to be replaced due to friction plate damage or I-beam failure.
During coal cake preparation, if any hammer liner fails, the hammer is lifted manually using a chain block. This process takes a minimum of 45 minutes per occurrence with result in production loss. (70MT Gross coke / Hour).
Also read: Can 75 meter tall steel chimney structures be dismantled without having a path for access?
Let’s list all activities and the time taken for stamping hammer lifting using a chain block.
| Steps | Activities | Type of Activity | Before |
| Step 1 | Reaches the man power to the site | Incidental | 5 |
| Step 2 | Equipment power supply isolation | Incidental | 3 |
| Step 3 | 2T Chain block to be shifted to the problamatic hammer. | Wasteful | 2 |
| Step 4 | Chain block upper hook to be fixed in clamping structure arrangement | Wasteful | 1 |
| Step 5 | Chain block load chain should be ensured sufficient length | Wasteful | 1 |
| Step 6 | Coal to be cleaned in hammer head clamp area | Wasteful | 2 |
| Step 7 | Chain block lower hook to be fix in hammer head clamp arrangement | Wrench | 2 |
| Step8 | Hammer to be lifted by using hand chain of chain block | Wrench | 15 |
| Step 9 | Hammer can be locked by locking pad mechanism | Wrench | 1 |
| Step 10 | Hammer can be locked by locking chain | Wrench | 2 |
| Step 11 | Chain block to load chain to be loosened for removing the lower hook | Wrench | 2 |
| Step 12 | Lower hook to be removed from hammer | Wasteful | 2 |
| Step 13 | Chain block to be removed clamping structure | Wasteful | 2 |
| Step 14 | Chain block to be shifted to allocated area | Wasteful | 2 |
| Step 15 | Equipment power supply normalization | Incidental | 2 |
| Step 16 | Hammer bottom lock can be done for all hammers | Wrench | 1 |
| Total time in Min | 45 | ||
Before Analysis Done Using a Waterfall Chart
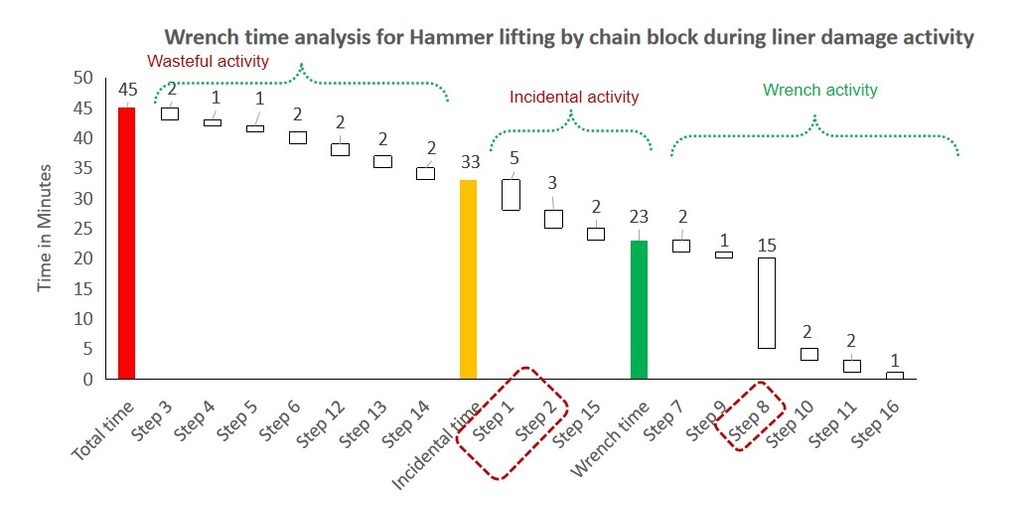
Stamping hammer lifting by chain block during liner damage activity takes 45 minutes for every occasions.
12min taken for wasteful activity in every occasions.
Action Taken
Modified winch mechanism provided on CAC trolley & individual pulley arrangement to be provided for each hammer.
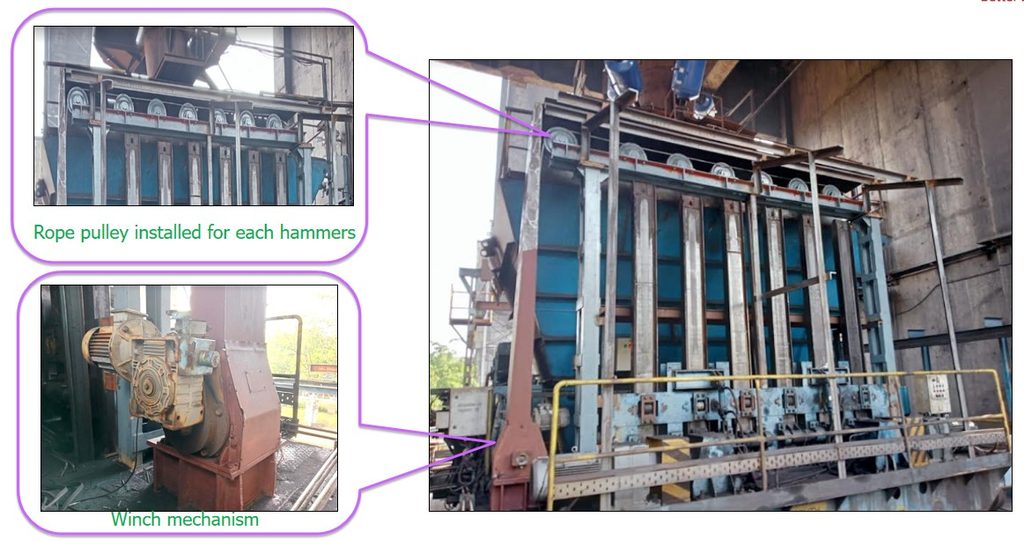
Obsolete Winch mechanism is used for this application, which is removed from WHRB#3 Damper valve. (WHRB – Waste Heat Recovery Boiler)
After Analysis
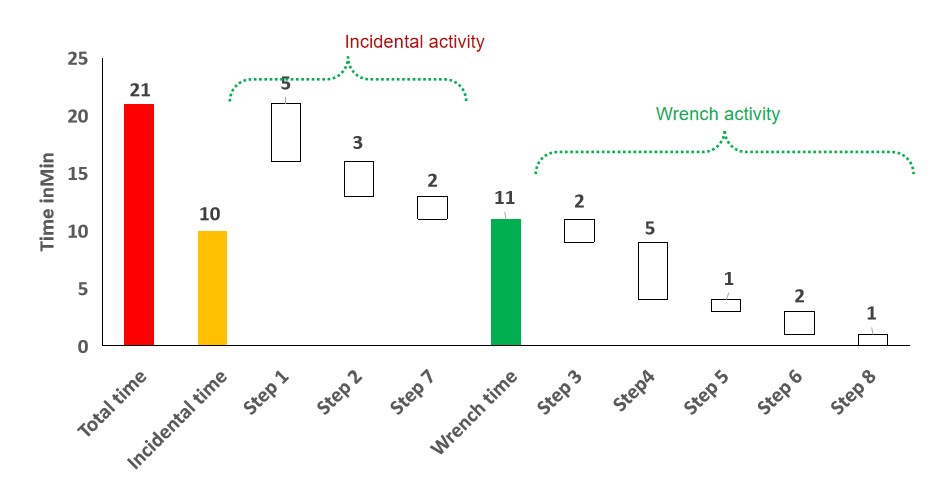
After eliminating the wasteful activities for Stamping hammer lifting activity time reduced from 45min to 21min for every occasions.
Cost savings
| S. No. | Description | Calculation | Value |
| 1 | Hammer lifting failures per month | Both stamping stations | 3 failures |
| 2 | Time saved per failure | — | 24 minutes |
| 3 | Total saved time per Month | 3 × 24 | 72 minutes |
| 4 | Approximate production delay considered per month | — | 60 minutes |
| 5 | Daily coke production | — | 1,400 MT |
| 6 | Hourly coke production | 1,400 ÷ 24 | 58.33 MT |
| 7 | Metallurgical coke price per MT | — | ₹30,100 |
| 8 | Production value per hour | 58.33 × ₹30,100 | ₹17.55 lakh |
| 9 | Estimated monthly production value protected | 60 minutes of production saved | ₹17.55 lakh |
Note: The estimated production value protected is based on 60 minutes of avoided production delay.
Types of Wrench Time Analysis:
- Walk-Around Wrench Time Analysis (Random Observations)
- Job-Based Wrench Time Analysis (Shadow Observations)
The main difference is :
| Walk-Around WTA | Job-Based WTA |
|---|---|
| Observes technicians performing different activities. | Observes one specific maintenance job. |
| Observations are made at random intervals. | Observes the job continuously from start to finish. |
| May take 1–8 hours. | Usually takes 30–60 minutes. |
| Helps identify general time losses across maintenance activities. | Helps identify the exact time taken and delays at each step of a job. |
| Example: Technicians are doing during a worksite in one occasion. | Example: Recording every activity involved in lifting a stamping hammer using a chain block. |
Conclusion
Through Wrench Time Analysis, we identified the time spent on each activity during stamping hammer lifting and found opportunities to eliminate wasteful activities. We modified the winch mechanism on the CAC trolley and provided individual pulley arrangements for each hammer. With this improvement, Reduced the hammer lifting time from 45 minutes to 21 minutes per occasion, saving 24 minutes each time. This practical and cost-effective modification helped us reduce production downtime and increase equipment availability.